

What Are the Most Common Long-Term Operating Challenges of MVR Evaporators in Chemical Wastewater Treatment?
MVR evaporators are widely used in chemical wastewater treatment, particularly for handling high-salinity wastewater, highly concentrated effluent, and wastewater that is difficult to treat through conventional processes. In many industrial applications, evaporation and concentration play an important role in wastewater volume reduction and zero liquid discharge (ZLD) systems.
The working principle of MVR is relatively straightforward. Mechanical vapor recompression technology recovers the secondary vapor generated during evaporation, compresses it to increase its temperature and pressure, and then reuses it as a heat source within the system. This reduces the demand for fresh steam compared with conventional evaporation processes. For chemical plants that require continuous operation, this energy-saving feature is particularly valuable.
However, the long-term performance of an MVR evaporator cannot be evaluated by evaporation capacity and theoretical energy consumption alone.
As water continuously evaporates, salts, inorganic compounds, and certain organic substances become increasingly concentrated. Problems that may appear insignificant in the original wastewater can gradually develop into scaling, corrosion, foaming, blockage, and increased equipment loads.
For chemical plants, the real question is not simply how often an MVR evaporator needs maintenance. It is understanding which factors make long-term operation more difficult and how these risks can be controlled through proper process design.
1. Scaling Is Often the First Major Challenge During Long-Term Operation
Chemical wastewater varies considerably in composition. However, high salt concentrations, elevated hardness, and inorganic compounds that readily form deposits are common challenges in many industrial applications.
During MVR operation, water continuously evaporates, causing non-volatile substances in the wastewater to become more concentrated. When certain salts reach supersaturation, crystallization may occur, allowing deposits to accumulate on heat transfer surfaces.
At the early stage, the equipment may continue operating normally. As scale gradually builds up, however, heat transfer efficiency decreases. The system may need to operate under a higher load to maintain the original evaporation capacity, resulting in increased energy consumption. If the problem continues, shutdowns for chemical or mechanical cleaning may become necessary.
This explains why some chemical plants only recognize the maintenance challenges of MVR systems after several months of operation.
Scaling is not simply a cleaning issue. It is closely related to feedwater quality, concentration ratio, operating temperature, and the final concentration target.
During the engineering design stage, the main scale-forming substances should therefore be identified through wastewater analysis. Based on the results, engineers can determine the appropriate pretreatment requirements and select a suitable evaporation and concentration process.
2. Why Should Corrosion Risks Not Be Evaluated by pH Alone?
Chemical plants commonly handle acids, alkalis, salts, and various chemical additives. As a result, the wastewater may have more complicated corrosion characteristics than ordinary industrial effluent.
Wastewater with a nearly neutral pH does not necessarily present a low corrosion risk. Chloride ions, certain inorganic salts, and other chemical components may become more aggressive under elevated temperatures and high-concentration conditions.
As water evaporates in an MVR system, some substances continue to accumulate. The concentrated liquid inside the equipment may therefore have significantly different characteristics from the original wastewater.
Material selection should not be based on raw wastewater pH alone. Heat exchangers, evaporators, pipelines, pumps, and sealing components all need to be evaluated according to the actual wastewater composition, operating temperature, concentration ratio, and corrosive substances. For wastewater containing high chloride concentrations, strong acids, or other aggressive chemical components, material compatibility should be addressed during project design rather than after corrosion problems appear.
3. Why Can Fluctuating Wastewater Quality Be More Difficult to Manage?
One characteristic of chemical manufacturing is that production conditions frequently change. A plant may manufacture one product today and switch to another tomorrow. Wastewater discharged from different production workshops may also contain different concentrations of salts, organic compounds, and suspended solids.
When these wastewater streams are mixed and sent directly into an MVR evaporator, the equipment must handle continuously changing feed conditions.
For example, a sudden increase in salt concentration may raise the risk of crystallization and scaling. An increase in organic substances or surfactants may contribute to excessive foaming. Rapid changes in feed flow can also cause fluctuations in the system's thermal load.
This is why equalization tanks and feedwater homogenization are important for stable MVR operation.
A properly designed treatment process generally follows a sequence such as:
Wastewater segregation → Equalization and homogenization → Pretreatment → Solid-liquid separation and oil removal → MVR evaporation and concentration → Condensate recovery or advanced treatment → Concentrate disposal By stabilizing the feedwater flow and composition as much as possible, the MVR system can operate under more predictable conditions.
4. Foaming May Be Overlooked but Can Affect the Entire Evaporation Process
Surfactants, organic compounds, and certain chemical additives in industrial wastewater may increase its tendency to foam during evaporation.
Excessive foaming is more than a visual operating issue. It can interfere with vapor-liquid separation and cause liquid droplet carryover, allowing contaminants to enter the secondary vapor system.
This becomes particularly important when the condensate is intended for reuse. Contaminant carryover may directly affect condensate quality and increase the requirements for subsequent treatment.
For chemical wastewater with a high foaming tendency, MVR design should therefore consider vapor-liquid separation, liquid level control, and foam management rather than focusing exclusively on evaporation capacity.
In some projects, the equipment itself may not show obvious mechanical faults, yet condensate quality and evaporation stability remain unsatisfactory. In such cases, the underlying problem may be related to feedwater characteristics and separation conditions rather than the vapor compressor.
5. The Condition of the Vapor Compressor Directly Affects Operating Costs
One of the key differences between MVR evaporators and conventional evaporation equipment is their reliance on a compressor to recompress secondary vapor.
When the compressor operates abnormally, the impact can extend beyond a single component and affect the thermal circulation of the entire system.
During long-term operation, several parameters require regular monitoring, including bearing condition, lubrication, vibration, electrical current, and operating temperature. If compressor performance deteriorates, the system may experience reduced evaporation capacity or increased energy consumption per unit of water evaporated.
Circulation pumps require similar attention.
Changes in pump flow rate and pressure can affect material circulation and heat transfer performance. Mechanical seal leakage, bearing wear, and impeller damage may eventually lead to unplanned shutdowns if they are not addressed in time.
For this reason, MVR maintenance should not begin only after an alarm or equipment failure occurs.
A more effective approach is to monitor operating data and identify abnormal trends. For example, under similar feedwater conditions, continuous changes in heat transfer temperature differences, gradually increasing compressor current, or abnormal circulation pump pressure may indicate scaling, blockage, or mechanical deterioration.
6. Higher Concentration Does Not Always Mean Better Performance
One issue that is easily overlooked in chemical wastewater MVR projects is the assumption that higher concentration is always desirable.
In theory, evaporation can continuously remove water and increase the concentration of the remaining wastewater. In actual engineering applications, however, maximizing concentration is not necessarily the most economical approach.
As concentration increases, wastewater viscosity, salt content, and crystallization risks may also change. Further concentration can make heat transfer, circulation, and concentrate discharge increasingly difficult.
Therefore, an MVR system needs a reasonable and clearly defined final concentration target.
For projects aiming at zero liquid discharge, engineers must also consider how the concentrated liquid will be handled after evaporation. Possible downstream processes may include further crystallization, solid-liquid separation, or other treatment and resource recovery methods. In other words, an MVR evaporator should be evaluated as part of the complete wastewater treatment process rather than as a standalone unit expected to handle every treatment challenge.
7. Proper Pretreatment Is the Key to Reducing Long-Term Maintenance
When equipment problems occur, many companies initially respond by increasing maintenance and cleaning frequency. However, more frequent cleaning does not necessarily address the underlying causes.
If the wastewater entering the MVR system contains excessive suspended solids, oil, or substances that readily cause scaling, even regular cleaning may not fundamentally improve operating conditions.
A more practical approach is to assign different treatment responsibilities to different process units.
For example, pretreatment can remove suspended solids, oil, and selected contaminants that may interfere with evaporation. Membrane systems can provide upstream concentration where the wastewater characteristics make them suitable. The MVR evaporator can then handle further evaporation and concentration, while the final concentrated liquid proceeds to crystallization, solid-liquid separation, or other appropriate treatment processes.
The goal is not to make the MVR evaporator handle every wastewater problem. It is to remove or control unsuitable substances before they enter the system, allowing the evaporator to perform the process it is designed for.
This approach can improve operating stability and make long-term maintenance costs easier to manage.
8. What Should Chemical Plants Evaluate When Selecting an MVR Evaporator?
When selecting an MVR evaporator, chemical plants should look beyond the initial equipment price and rated evaporation capacity.
The most important consideration is whether the system is compatible with the actual wastewater characteristics and treatment requirements.
| Evaluation Area | Key Considerations |
|---|---|
| Raw wastewater quality | Salt concentration, COD, SS, hardness, chloride content, and specific contaminants |
| Pretreatment | Whether scaling, blockage, and foaming risks can be reduced before evaporation |
| Operating conditions | Feed flow rate, temperature, pressure, and target concentration |
| Material selection | Compatibility with actual corrosive substances and long-term operating conditions |
| Vapor compressor | Operating stability, energy consumption, and maintenance requirements |
| Automatic control | Reliable monitoring and control of temperature, pressure, liquid level, and flow rate |
| Concentrate treatment | How the concentrated liquid will be handled after evaporation |
| Maintenance accessibility | Convenience of cleaning, inspection, repairs, and replacement of key components |
These factors are closely interconnected.
For example, inadequate pretreatment may lead to scaling. As scale accumulates, heat transfer efficiency decreases, potentially affecting the operating load of the compressor and circulation system. The result may be higher energy consumption and more frequent maintenance. This means that part of the long-term maintenance cost of an MVR system is already determined during the project design stage.
9. WTEYA Focuses on the Complete Industrial Wastewater Treatment System
For chemical wastewater applications, an MVR evaporator should rarely be evaluated as an isolated piece of equipment.
WTEYA focuses on the overall process design of industrial wastewater treatment projects, taking into account pretreatment, concentration, evaporation, and downstream concentrate treatment. The appropriate process route depends on the specific wastewater characteristics and project objectives.
For different types of chemical wastewater, process selection needs to consider salt composition, organic content, corrosivity, treatment capacity, and the requirements for water reuse or zero liquid discharge.
The purpose of this system-oriented approach is to keep the feedwater entering the MVR system under more controllable conditions while preventing the evaporation unit from handling problems that could have been addressed during pretreatment. For chemical plants requiring long-term continuous operation, this approach is often more important than focusing solely on the initial equipment specifications.
Conclusion:
The main challenge of using MVR evaporators for chemical wastewater treatment is not simply whether the equipment can evaporate water. During long-term operation, scaling, corrosion, foaming, feedwater fluctuations, mechanical wear, and concentration limits can all affect system efficiency and maintenance costs.
These problems are not isolated. In many cases, the root causes of equipment difficulties can be traced back to wastewater characteristics and process design decisions.
A reliable MVR system for chemical wastewater should therefore start with a thorough analysis of the raw wastewater. Pretreatment, evaporation, concentrate handling, and continuous monitoring of key operating parameters should all be considered as part of an integrated treatment strategy.
Selecting the right equipment is only the first step. What ultimately determines whether an MVR evaporator can operate reliably over the long term is whether the entire treatment system is designed to handle the actual characteristics of the chemical wastewater.
Why Partner with WTEYA?
• Nearly 20 years of industry experience
• Trusted by global leaders including Foxconn, Huawei, Ganfeng Lithium, Ronbay Technology
• 100+ success cases worldwide
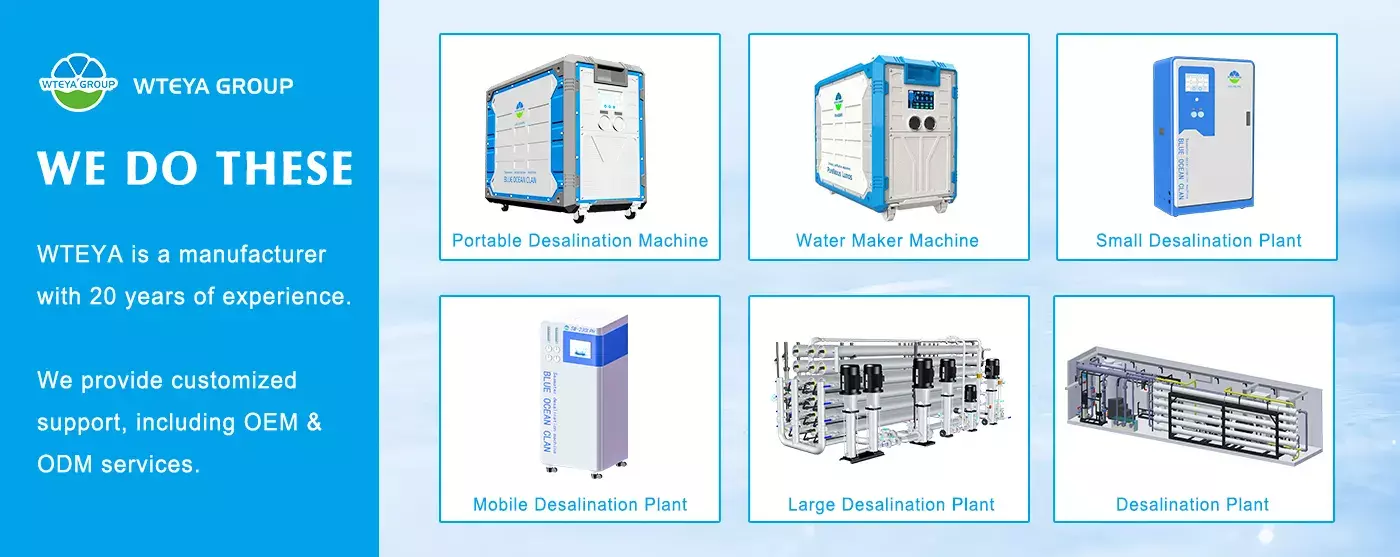
• OEM & ODM customization available
Become a WTEYA Distributor!
We are expanding global partnerships:
• Preferential policies
• Professional training
• Full technical support
Let us help you achieve exceptional water quality and operational sustainability!
📲 WhatsApp: +86-1800 2840 855
📧 Email: info@wteya.com
🌐 Website: www.wteya.com
Previous: Leachate Treatment: Full-Process Approach for Australia
Next: No More