

What Is the Role of an MVR Evaporator in Wastewater Treatment?
An MVR evaporator is an evaporation system that uses mechanical vapor recompression technology to recover and reuse the heat contained in secondary vapor. In industrial wastewater treatment, it is commonly used for high-salinity wastewater, high-concentration wastewater, and concentrate generated by membrane treatment processes. By evaporating water and concentrating dissolved substances, an MVR evaporator reduces wastewater volume and prepares the remaining liquid for subsequent crystallization and zero liquid discharge (ZLD) processes.
Compared with conventional evaporation systems, an MVR evaporator uses a vapor compressor to increase the pressure and temperature of secondary vapor. The compressed vapor is then returned to the heating system, where its recovered heat supports further evaporation. This heat-reuse mechanism reduces the demand for fresh steam, making MVR technology a potential energy-saving option for industrial wastewater projects that require continuous operation.
1. How Does an MVR Evaporator Work?
The working process of an MVR evaporator mainly involves three stages: evaporation, secondary vapor compression, and heat recovery.
Wastewater enters the evaporator and absorbs heat through the heat exchanger. Once the water reaches its boiling point, part of it evaporates and forms secondary vapor. A vapor compressor then raises the vapor pressure, increasing its saturation temperature. The compressed vapor returns to the heat exchange system and supplies the heat required for further evaporation. After releasing its heat, the vapor condenses into water.
Through this process, the system repeatedly reuses the thermal energy contained in the secondary vapor.
Typical process flow: Wastewater feed → Heating and evaporation → Secondary vapor generation → Vapor compression → Heat reuse → Condensation and water recovery.
An MVR system usually requires an external heat source during startup. Once stable operating conditions are established, mechanical vapor recompression becomes the primary mechanism for circulating and reusing heat. Actual energy consumption depends on factors such as treatment capacity, feed concentration, evaporation temperature, boiling point elevation, and compressor efficiency. These parameters should be evaluated for each project.
2. What Are the Main Functions of an MVR Evaporator in Wastewater Treatment?
MVR evaporators are mainly used for wastewater concentration, volume reduction, and downstream treatment preparation in industrial wastewater systems.
First, continuous evaporation removes water and increases the concentration of salts and other non-volatile substances. This reduces the volume of liquid requiring further treatment. For high-concentration streams generated by membrane separation, an MVR evaporator can provide additional concentration before the liquid enters a crystallization process.
Second, MVR technology can serve as an important component of a zero liquid discharge system. Water is evaporated and condensed for recovery, while the concentrated liquid proceeds to crystallization or another suitable end-treatment process.
The main application areas include:
High-salinity wastewater: Evaporates water to increase salt concentration and reduce liquid volume.
High-concentration industrial wastewater: Reduces wastewater volume and lowers the burden on downstream treatment.
Membrane concentrate treatment: Further concentrates liquid streams generated by reverse osmosis or other membrane processes.
Zero liquid discharge systems: Works with crystallizers and other equipment to support the final stages of wastewater treatment.
Salt concentration: Prepares concentrated solutions for subsequent crystallization and solid-liquid separation.
It is important to understand that an MVR evaporator primarily performs separation and concentration. It cannot replace every upstream process required to remove or control contaminants.
3. Which Types of Industrial Wastewater Can Be Treated with MVR Evaporation?
MVR evaporation is generally considered for wastewater with high salinity, high contaminant concentrations, or a need for further concentration and volume reduction. Its suitability depends on the wastewater composition and operating conditions.
Industries such as chemical manufacturing, electroplating, pharmaceuticals, lithium battery production, and textile dyeing may generate wastewater containing high salt concentrations or contaminants that are difficult to remove through conventional treatment alone. Depending on the water quality, these streams may undergo pretreatment and membrane separation before the concentrate is sent to an MVR evaporator.
The main treatment challenges vary by wastewater type. High-hardness wastewater requires effective scale control. Wastewater containing substantial organic matter may require measures to manage foaming and high viscosity. Wastewater with elevated chloride concentrations requires careful assessment of corrosion risks in relation to operating temperature, concentration, and pH.
For these reasons, MVR evaporators should not be selected solely on the basis of industry classification. Process design must be based on actual wastewater characteristics and the treatment objectives of the project.
4. Why Does an MVR Evaporator Require Pretreatment?
Industrial wastewater usually requires appropriate pretreatment before entering an MVR evaporation system. Suspended solids, oils, hardness ions, and scale-forming compounds can become increasingly concentrated as water evaporates. If these substances are not adequately controlled, they may cause heat transfer surface fouling, reduced evaporation efficiency, excessive foaming, or equipment corrosion.
Depending on the wastewater characteristics, pretreatment may include coagulation and sedimentation, dissolved air flotation, filtration, softening, or oxidation. The purpose is to reduce contaminants that could interfere with stable evaporator operation.
Some industrial wastewater systems also use membrane processes such as reverse osmosis (RO) or nanofiltration (NF) to recover water before sending the resulting concentrate to the MVR evaporator.
A typical treatment route may be arranged as follows:
Pretreatment → Advanced treatment → Membrane separation → MVR evaporation → Crystallization.
The actual process flow should be adjusted according to wastewater composition, treatment capacity, water recovery targets, and final discharge or disposal requirements.
5. How Is MVR Evaporation Used in Zero Liquid Discharge Systems?
A zero liquid discharge project aims to maximize water recovery and manage the remaining concentrated liquid or solid residues. In many ZLD systems, the MVR evaporator is installed toward the end of the treatment process to further concentrate high-salinity wastewater or membrane concentrate.
During evaporation, water becomes vapor and is subsequently condensed into recovered water. Depending on its quality, the condensate may be reused directly or sent for additional treatment. Salts and other non-volatile substances remain in the concentrated liquid and may undergo further crystallization, depending on project requirements.
The main contributions of MVR technology to ZLD systems are wastewater volume reduction, increased concentration, thermal energy recovery, and integration with downstream crystallization.
However, evaporation does not eliminate contaminants. Instead, it concentrates them in the residual liquid or solid products. The treatment and disposal of crystallized salts and residual mother liquor must therefore be considered as part of the overall ZLD system design.
6. What Factors Should Be Considered When Designing an MVR Evaporation System?
The performance of an MVR evaporator depends heavily on wastewater characteristics and operating conditions. Several factors should be evaluated during equipment selection and process design.
Feedwater quality: Analyze salinity, chemical oxygen demand (COD), suspended solids, hardness, and other relevant contaminants.
Treatment capacity: Determine the required evaporation rate and overall equipment capacity based on the wastewater flow and target concentration.
Scaling potential: Evaluate salt solubility and precipitation behavior throughout the concentration process to identify the risk of deposits forming on heat transfer surfaces.
Corrosion resistance: Select suitable equipment materials based on chloride concentration, pH, operating temperature, and the corrosive properties of the wastewater.
Evaporation conditions: Establish the appropriate operating temperature, concentration ratio, and expected boiling point elevation.
Downstream treatment: Define the intended treatment or disposal routes for concentrated liquid, crystallized salts, and recovered condensate.
For wastewater with complex compositions or significant variations in quality, laboratory testing and, where necessary, pilot-scale trials can help establish suitable process conditions and equipment parameters before full-scale implementation.
7. WTEYA MVR Evaporators and Industrial Wastewater Treatment Solutions
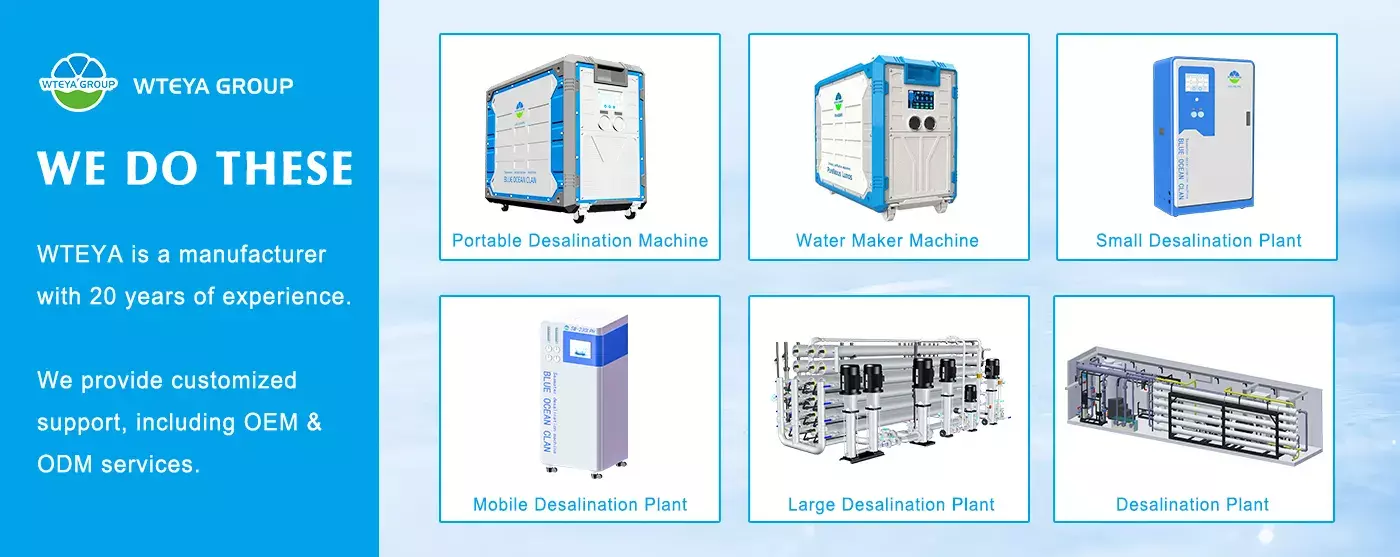
WTEYA specializes in industrial wastewater treatment and evaporation concentration technologies. Based on wastewater characteristics, treatment capacity, and discharge requirements, WTEYA can develop integrated process solutions combining pretreatment, membrane separation, MVR evaporation, and crystallization.
In practical engineering applications, an MVR evaporator does not operate in isolation. Its performance depends on how well it integrates with upstream treatment processes and downstream residue management. A wastewater-specific process design can help address scaling, corrosion, and operating stability while supporting wastewater volume reduction and zero liquid discharge objectives for high-salinity industrial wastewater.
Conclusion:
The primary role of an MVR evaporator in wastewater treatment is to use mechanical vapor recompression to recover heat while concentrating and reducing the volume of high-salinity wastewater, high-concentration wastewater, or membrane concentrate.
In industrial zero liquid discharge systems, MVR evaporation can be integrated with pretreatment, membrane separation, and crystallization to form a coordinated treatment process. For each project, the suitability of MVR technology and the required equipment configuration should be determined through a comprehensive assessment of wastewater quality, treatment capacity, evaporation conditions, energy requirements, and final residue management.
Why Partner with WTEYA?
• Nearly 20 years of industry experience
• Trusted by global leaders including Foxconn, Huawei, Ganfeng Lithium, Ronbay Technology
• 100+ success cases worldwide
• OEM & ODM customization available
Become a WTEYA Distributor!
We are expanding global partnerships:
• Preferential policies
• Professional training
• Full technical support
Let us help you achieve exceptional water quality and operational sustainability!
📲 WhatsApp: +86-1800 2840 855
📧 Email: info@wteya.com
🌐 Website: www.wteya.com
Previous: Desalination for Island Resorts: Reliable Fresh Water Supply
Next: No More